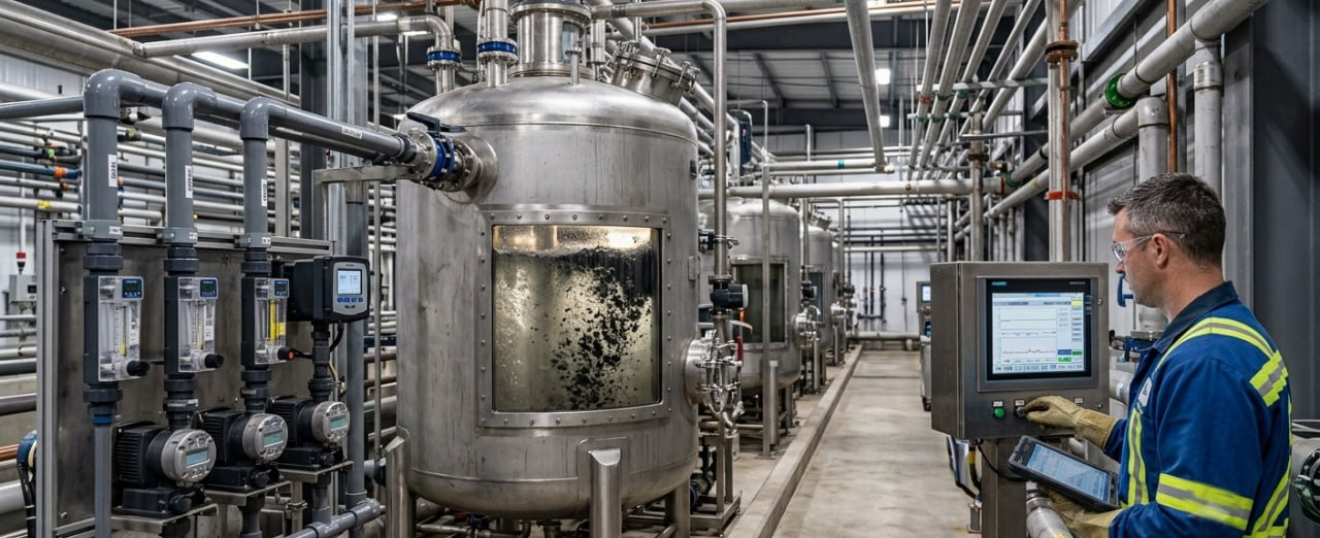
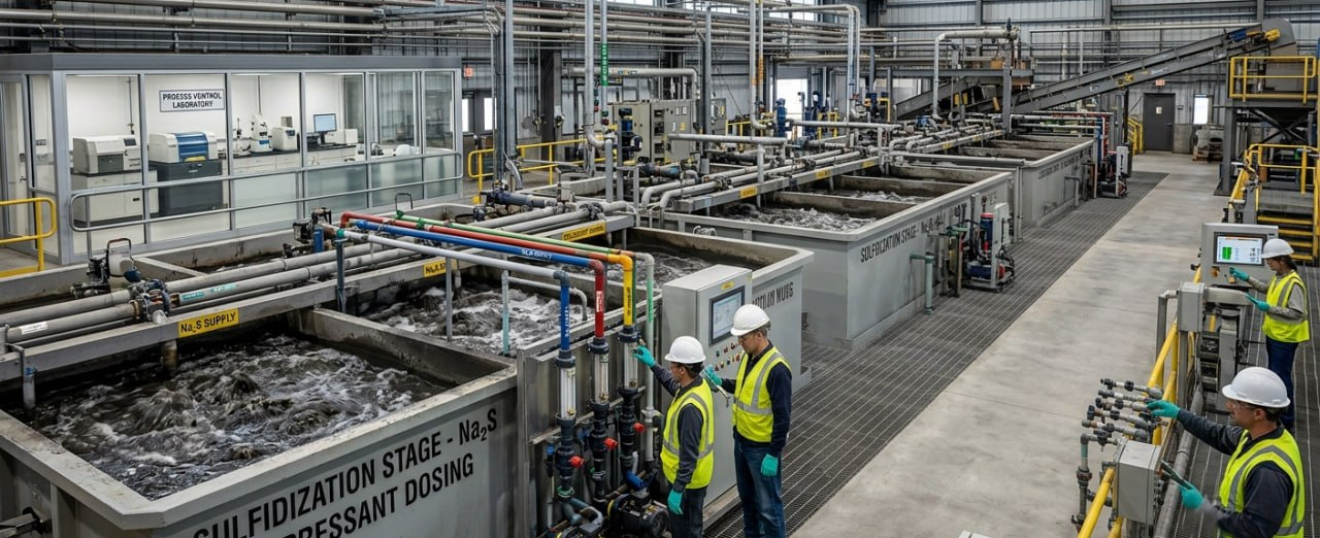
In modern chemical manufacturing, water is both a vital process utility and a growing compliance challenge. Implementing a Zero Liquid Discharge (ZLD) system allows plants to recover up to 95–98% of process water for reuse, eliminating wastewater discharge and drastically reducing freshwater intake.
While ZLD relies heavily on mechanical equipment such as Reverse Osmosis (RO) membranes and evaporators the success of these systems is fundamentally driven by intelligent chemical conditioning. Without precise chemical treatment, high-tech hardware quickly succumbs to scaling, biofouling, and operational downtime.
The Key Chemical Stages in a ZLD Process Chain
A reliable ZLD system integrates targeted chemical treatment across every phase of the water recycling loop:
A. Pre-Treatment: Coagulation & Flocculation
Before water enters high-pressure membranes, suspended solids and colloids must be removed.
· Coagulants (alum, ferric salts) neutralize particle charges to initiate aggregation.
· Polymer Flocculants aggregate micro-flocs into large, settleable masses.
· Benefit: Protects expensive membranes from physical abrasion and premature fouling.
B. Precision pH Control
pH is the single most critical variable governing solubility in wastewater streams.
· High pH (using Caustic Soda / Lime): Promotes hardness precipitation (calcium and magnesium removal) prior to thermal concentration.
· Neutral/Adjusted pH: Keeps silica and heavy metals in manageable phases during treatment.
C. Scale & Biofouling Inhibitors
Membranes operating at high water recovery rates (80–90%) are highly vulnerable to scaling from sulfates, carbonates, and silica.
· Anti-Scalants: Threshold chemicals that keep sparingly soluble salts suspended in concentrated brine.
· Biocides (Sodium Hypochlorite): Prevent organic biofilms from clogging membrane pores.
Economic Benefits of Chemically Optimized ZLD
Integrating optimized chemical treatment into your ZLD infrastructure delivers clear business advantages:
· Lower Operating Costs (OPEX): Prevents scale formation, reducing costly membrane replacement and chemical cleaning frequencies.
· Maximum Water Recovery: Cuts freshwater procurement costs while maintaining consistent feed quality for chemical processing.
· Regulatory & ESG Compliance: Ensures zero liquid discharge liability, aiding compliance with environmental regulations in target export markets (Pakistan, Turkey, CIS).
Why Partner with PKS Chemicals?
At PKS Chemicals, we support chemical manufacturers and industrial buyers with high-purity, export-grade chemicals essential for industrial water treatment and process recycling:
· Verified Quality & Purity: Consistent active assay for reliable, automated chemical dosing.
· Full Export Documentation: Detailed COA, TDS, SDS, and Certificate of Origin with every shipment.
· Export-Ready Packaging: Moisture-resistant, heavy-duty industrial packaging that preserves chemical integrity during transit.
Optimize Your Process Water Recycling
Eliminate scaling, protect your equipment, and maximize water recovery in your plant.
Contact PKS Chemicals today to discuss your chemical requirements and request technical specifications for your water treatment operations.