In the international trade of industrial raw materials, arriving on time is only half the measure of logistics success. The critical question for plant managers and procurement heads is whether the chemical arrives with its original concentration, purity, and physical stability intact.
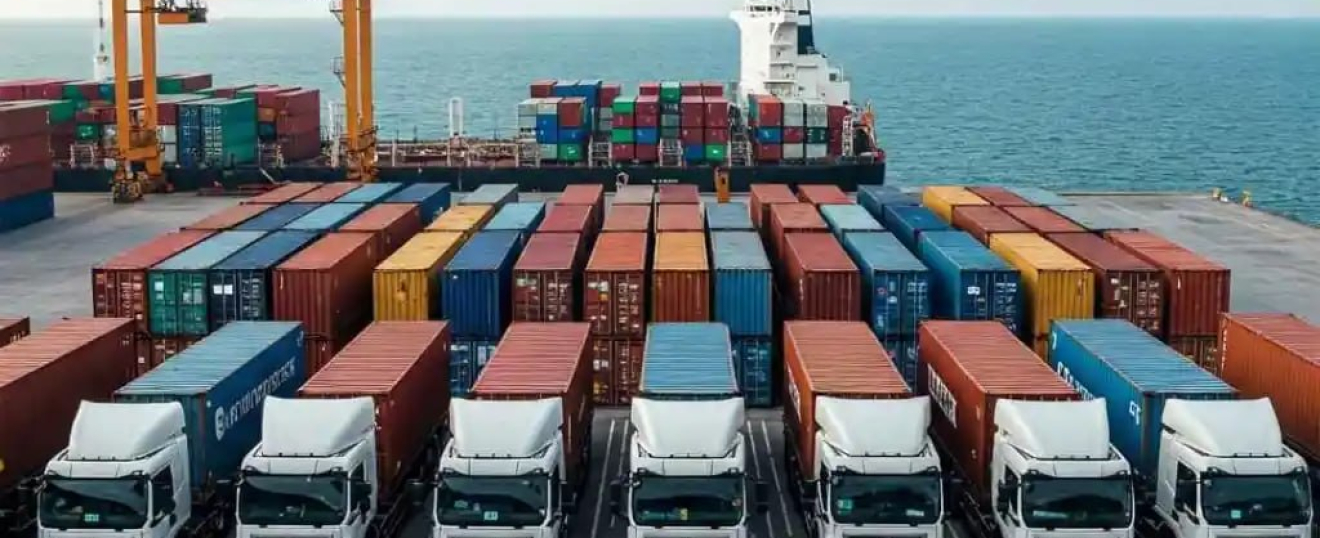
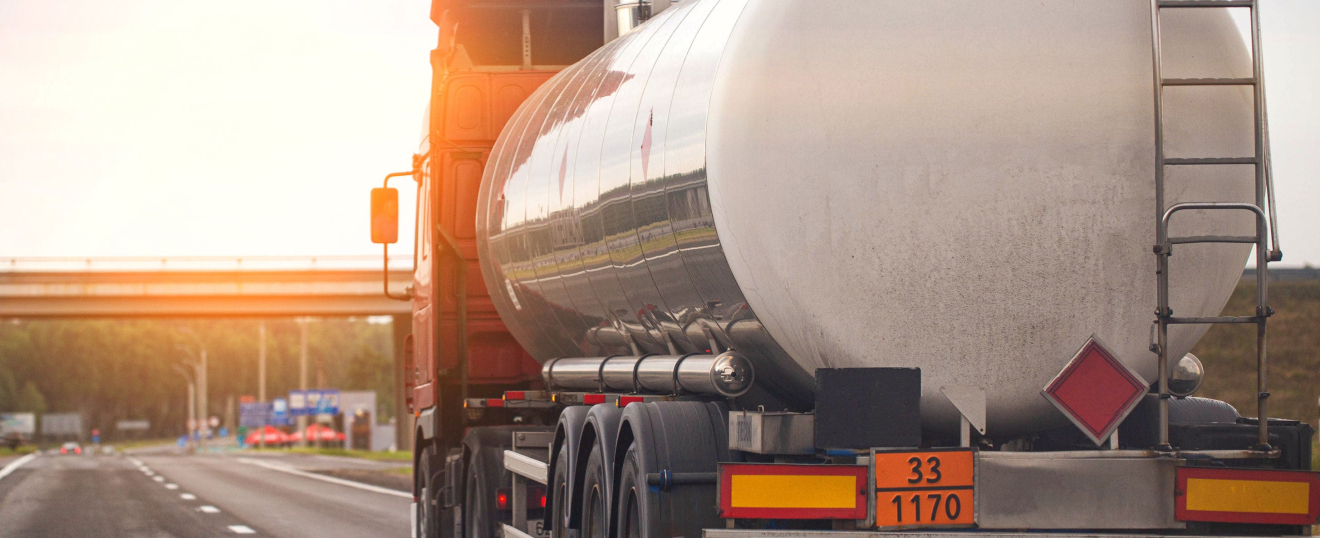
For high-demand, reactive commodities such as Caustic Soda Flakes and Sodium Sulfide Flakes, long-distance transit across maritime routes (IMDG) or overland trucking corridors (ADR) introduces significant environmental and handling risks. Extreme temperature swings, relative humidity, prolonged warehouse dwell times, and unmonitored handling can trigger severe degradation or invite fraudulent tampering.
Protecting cargo value requires an integrated defense strategy combining multi-barrier packaging, strict chain-of-custody controls, and disciplined receiving protocols.
Primary Causes of Chemical Quality Loss
Quality loss during cross-border transit is rarely accidental. It follows predictable physical and chemical degradation pathways when containment standards are compromised:
A. Moisture Absorption and Deliquescence
Many industrial alkalis and salts are strongly hygroscopic they actively draw moisture vapor directly out of ambient air.
When packaging allows humid air to seep in, materials begin to dissolve on their surface, creating a sticky film.
As transit temperatures fluctuate, these dissolved surfaces dry out and recrystallize, fusing loose flakes into dense, rock-solid agglomerates that clog plant hoppers and resist standard dissolving procedures.
B. Atmospheric Degradation (Air Exposure)
Prolonged contact with ambient air alters the fundamental purity of reactive chemicals:
Reactive alkalis slowly absorb carbon dioxide from air trapped inside the packaging or leaking through micro-punctures. This converts active material into inert carbonates, lowering the usable active concentration and introducing insoluble residues that foul plant filtration systems.
Sulfur-bearing compounds oxidize under trapped heat and humidity, generating unwanted byproducts that impair performance in precision applications such as textile dyeing and leather tanning.
C. Container Rain and Condensation
During maritime transit or cross-border trucking through fluctuating day-night temperatures, air inside enclosed metal shipping containers reaches its dew point. Moisture condenses on the container ceiling and walls, dripping onto cargo pallets a phenomenon known as “container rain.” If outer packaging lacks moisture barriers, bags weaken, tear, and admit contaminated water.
Multi-Layer Packaging: The First Line of Defense
Standard single-layer bags cannot protect reactive industrial chemicals over long logistics cycles. Packaging must adhere strictly to United Nations (UN) certified packaging guidelines featuring layered protection:
· Heavy-Duty Polyethylene (PE) Inner Liners: The inner liner must be manufactured from virgin polymer resins with sufficient gauge thickness to create a continuous moisture and vapor seal. Recycled films with micro-porosity must be strictly rejected.
· Hermetic Heat Sealing: Traditional mechanical cable ties or string stitches allow atmospheric gas exchange. The inner liner must be thermally welded or heat-sealed to completely isolate the cargo from ambient air.
· Laminated Woven Polypropylene (PP) Outer Sacks: The outer layer provides physical tear and puncture resistance during container stuffing, palletizing, and border handling, complete with UV-stabilized coatings to withstand direct sunlight exposure at terminals.
· Industrial Container Desiccants: Placing high-absorption desiccant poles inside shipping containers active throughout the voyage neutralizes ambient humidity and prevents condensation droplets from contacting cargo.
Preventing Chemical Adulteration and Cargo Fraud
Beyond environmental degradation, chemical adulteration such as deliberate material dilution with cheaper inert salts, bag substitution, or unauthorized partial unloading poses severe financial and production hazards.
A transparent, tamper-evident supply chain eliminates these vulnerabilities:
High-Security ISO Bolt Seals
Every container or road transport unit must be locked with sequentially numbered, tamper-evident high-security bolt seals immediately after factory loading. The seal identification number must be permanently printed on the Bill of Lading, Road Waybill, and Packing List. Any mismatched or damaged seal at the destination flags unauthorized entry.
Indelible Batch Imprints on Every Unit
Generic, unmarked sacks encourage pilferage and counterfeit substitution. Legitimate chemical suppliers print indelible production details directly onto each individual bag, including:
· Batch/Lot number
· Production and expiration dates
· UN packaging performance mark
· Net and gross weight
Tamper-Evident Stretch Hooding
Palletized cargo should be sealed under high-tension, opaque or printed stretch hooding film, reinforced with security perimeter strapping and tamper-evident void tape. This guarantees that no individual sacks can be removed or swapped mid-transit without visibly tearing the outer barrier.
Documentation and Pre-Shipment Verification
A Certificate of Analysis (COA) is only dependable when it directly corresponds to the physical batch loaded into the transport unit.
Safeguard Measure | Standard Procedure | Procurement Benefit |
Batch-Matched Testing | Direct sampling from the finished batch prior to packaging | Confirms laboratory purity aligns with physical dispatch |
Independent Third-Party Inspection | Deployment of neutral inspection agencies (e.g., SGS) at origin | Verifies weight, assay, packaging integrity, and container seals |
Retained Reference Samples | Storage of vacuum-sealed counter-samples at the manufacturing plant | Provides verifiable evidence for arbitration in case of disputes |
Receiving Protocols for In-Plant Quality Assurance
Receiving teams should follow a standardized four-step check before accepting imported chemical cargo into factory storage:
· Verify Exterior Seals: Photograph container doors and match the bolt seal code against the original shipping documentation before cutting the seal.
· Inspect Container Internal Environment: Check for moisture marks, chemical odors, torn pallets, or white powder dust that might indicate broken bags.
· Inspect Physical Packaging: Confirm that inner liners remain hermetically sealed, flexible, and free of moisture beads or caking.
· Standard Laboratory Assay Check: Take composite cross-sectional samples from random pallets across the shipment and run immediate titration assays to confirm active purity against the supplier’s batch COA before discharging into bulk silos.
Engineering Purity into Every Mile
Preventing adulteration and transit degradation requires deliberate engineering rather than good luck. By combining robust multi-barrier packaging, automated thermal sealing, batch traceability, and tamper-evident container locks, industrial manufacturers can eliminate quality disputes and avoid production downtime.
At PKS Chemical, raw materials such as Caustic Soda and Sodium Sulfide are prepared under strict quality assurance standards, verified batch-by-batch with authentic documentation. Whether moving via direct full truckloads, ocean containers, or our Multi-Buyer Shared Container consolidation service, your cargo arrives factory-ready and uncompromised.
Protect your production line with certified, tamper-evident chemical sourcing. Contact the PKS Chemical logistics team to review packaging specifications for your target destination.